
The Chemistry Behind Stainless Steel Performance: A Technical Guide to Industrial Surface Treatment
Stainless steel is selected for its corrosion resistance, durability and suitability for demanding industrial environments. Yet even a correctly specified stainless steel grade can perform poorly if its surface has been contaminated, oxidised or inadequately treated during manufacturing.
Welding, machining, forming and heat treatment can all alter the surface condition. Residual oils, embedded iron, weld heat tint and oxide scale can affect the effectiveness of subsequent treatments and compromise the finished component.
This is where industrial surface treatment chemistry becomes critical.
From electropolishing electrolytes and acid pickling solutions to alkaline degreasers, passivating chemicals and contamination test kits, each chemical system performs a distinct function.
Understanding these differences allows manufacturers to select suitable treatments, establish controlled processes and achieve consistent surface quality.
Why Stainless Steel Surface Chemistry Matters
The corrosion resistance of stainless steel depends largely on the formation of a very thin, chromium-rich passive oxide film at its surface.
This film forms naturally when a clean stainless steel surface is exposed to an environment containing sufficient oxygen or other suitable oxidising species. Although only a few nanometres thick, it provides an important barrier against corrosion.
However, the condition of the underlying metal is just as important as the passive film itself.
During fabrication, several changes may occur:
Welding and heat treatment can produce oxide scale and heat tint, with chromium depletion immediately beneath the oxidised surface.
Machining and forming can introduce cutting oils, lubricants and other organic residues.
Mechanical handling and abrasive operations can transfer carbon steel particles or free iron onto the stainless steel.
Inadequate cleaning can leave chemical residues that interfere with subsequent processing.
The objective of chemical surface treatment is not simply to make stainless steel look cleaner. It is to produce a surface condition appropriate for the component's intended service environment.
1. Degreasing: Preparing the Surface for Chemical Treatment
Before electropolishing, pickling or passivation, the stainless steel surface must be sufficiently free from oils, greases and other contaminants.
Organic residues can interfere with the wetting of the metal by treatment solutions, producing inconsistent chemical contact and potentially leaving areas inadequately processed.
Industrial degreasing systems commonly use alkaline or acidic formulations, selected according to the contamination present, material compatibility and downstream treatment.
Alkaline Degreasing
Alkaline cleaners are widely used to remove machining oils, lubricants and workshop soils.
Their cleaning action may involve a combination of surfactant activity, emulsification, dispersion and, where the chemistry permits, saponification of suitable fatty contaminants.
Depending on the formulation and equipment, cleaning may be performed by immersion, spray or electrochemical methods.
Anopol's Degreaser 6 is an alkaline cleaning product intended for immersion or electrochemical degreasing applications.
Acid Cleaning
Acid cleaning products may be appropriate where surface contamination includes certain inorganic deposits or light oxides.
Anopol's chemical range includes Cleaner C, an acid degreaser for stainless steel, and Cleaner CX, designed for applications involving light oxides and spot-weld-related residues.
The choice between acidic and alkaline cleaning should depend on the nature of the contamination rather than treating the products as interchangeable.
Effective pre-cleaning helps establish a consistent starting condition for subsequent surface treatment.
2. Electropolishing Electrolytes: Controlled Electrochemical Metal Removal
Electropolishing is an electrochemical finishing process in which the workpiece acts as the anode within an electrolytic cell.
When an appropriate direct current is applied, metal dissolves from the component's surface into the electrolyte.
Under suitable operating conditions, microscopic surface projections can dissolve preferentially, producing a levelling effect that reduces surface roughness.
Electropolishing can also remove fine burrs, reduce surface contamination and produce a bright finish, although the achievable result depends on the initial surface condition, alloy and processing parameters.
The Role of the Electrolyte
The electrolyte is central to the process.
It provides ionic conductivity and establishes the chemical environment required for controlled anodic dissolution.
Commercial stainless steel electropolishing systems commonly use formulations based on phosphoric and sulphuric acids, although the precise composition of proprietary products must be confirmed from their technical documentation.
The behaviour of the process depends on several interacting variables:
Electrolyte composition and condition
Applied current density and voltage
Solution temperature
Treatment duration
Workpiece geometry and electrical contact
Cathode arrangement and current distribution
Dissolved metal content and bath contamination
These variables influence material removal, levelling, brightness and process consistency.
Importantly, electropolishing is not a universal method of eliminating all surface defects. Deep scratches, significant weld irregularities and inaccessible geometries may require preparation or alternative treatment.
Electropolishing Different Stainless Steel Grades
Austenitic, ferritic and martensitic stainless steels have different metallurgical compositions and electrochemical characteristics.
Consequently, an electrolyte suitable for one family of stainless steels may not deliver the same results on another.
Anopol supplies several specialist electropolishing products:
Anopol 66: An electrolyte for ferritic, martensitic and austenitic stainless steels.
Anopol 66A: A top-up product for Anopol 66 electrolyte systems.
Anopol 65: A specialist electrolyte for large-vessel applications and austenitic stainless steels.
Anopol 70: An electrolyte developed for ferritic and martensitic stainless steels.
Anopol 30: A dedicated electropolishing electrolyte for copper-based alloys.
Selecting the correct electrolyte requires consideration of the material grade, component geometry, existing surface condition and required finish.
For manufacturers operating in-house electropolishing facilities, maintaining electrolyte condition is equally important. Changes in chemical composition and dissolved metal concentration can affect process behaviour over time.
3. Acid Pickling: Removing Oxide Scale and Chromium-Depleted Material
Welding and heat treatment can cause substantial changes to the surface of stainless steel.
During welding, elevated temperatures promote oxidation. The resulting coloured oxide film is commonly known as heat tint.
As chromium participates in oxide formation, a chromium-depleted region can develop immediately beneath the oxide layer.
This region may exhibit reduced corrosion resistance compared with the unaffected parent material.
Simply removing the visible colour does not necessarily remove the underlying chromium-depleted material.
How Chemical Pickling Works
Pickling uses an appropriately formulated chemical solution to remove oxide scale and a controlled amount of underlying surface metal.
Traditional stainless steel pickling formulations frequently contain nitric and hydrofluoric acids, although alternative chemical systems also exist.
The treatment is intended to remove detrimental surface oxides and expose metal capable of developing a suitable passive film.
Pickling can be particularly important for:
Welded stainless steel fabrications
Heat-treated components
Process vessels and tanks
Stainless steel pipework
Components exposed to demanding corrosive environments
The required treatment depends on alloy composition, oxide condition and the service requirements of the component.
Why Stainless Steel Grade Matters
Not all stainless steels respond identically to pickling chemistry.
Austenitic stainless steels, including commonly used 304 and 316 grades, differ significantly from ferritic and martensitic 400-series grades.
Certain grades may be more susceptible to excessive acid attack, surface etching or localised damage under unsuitable processing conditions.
Anopol's range includes:
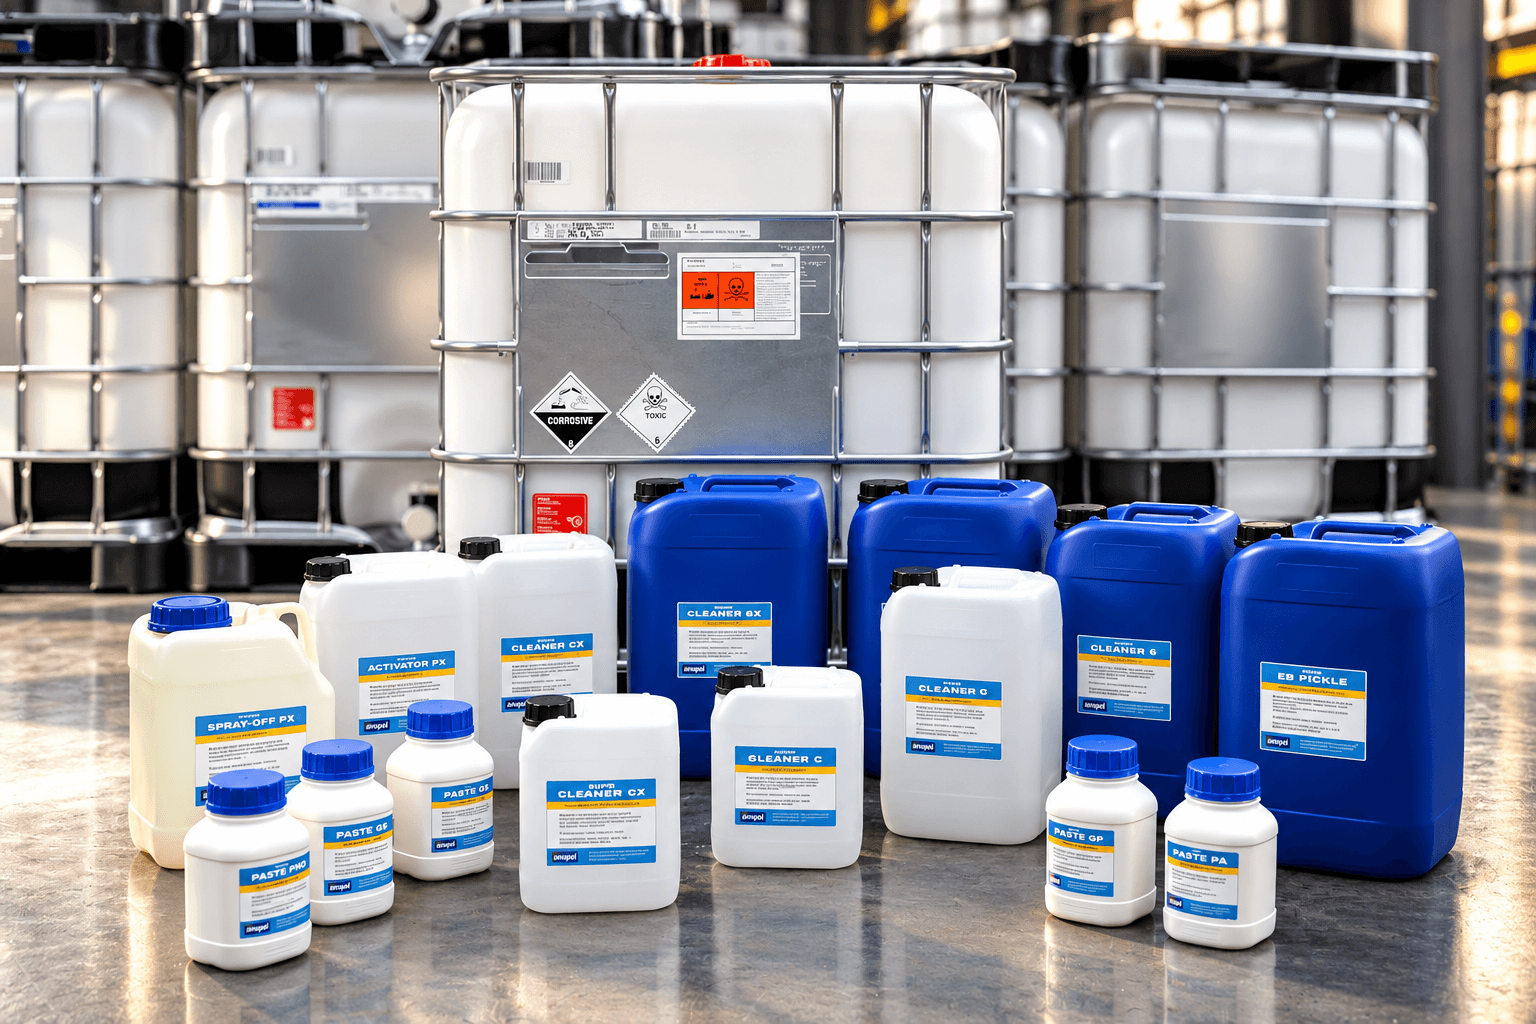
EB Pickle: An acid pickling solution developed for austenitic stainless steels.
Fluorinox: A concentrated pickling solution for demanding austenitic stainless steel applications.
Fluorinox 49: A lighter variant within the Fluorinox range.
CRB Pickle: A specialist solution for removing heat-treatment oxide scale from 400-series stainless steels.
AC Additive: A top-up product intended for Fluorinox pickling systems.
Chemical selection must be supported by the appropriate technical instructions and consideration of material compatibility.
Excessive exposure to pickling chemistry can damage the surface rather than improve it. Controlled processing and effective post-treatment rinsing are therefore essential.
4. Pickling Pastes and Gels: Localised Treatment of Welds and Fabrications
Immersion pickling is not always practical.
Large vessels, installed pipework, structural fabrications and individual welds may require treatment in specific areas rather than across the entire component.
Pickling pastes and gels allow chemical treatment to be applied locally.
Their viscosity helps retain the formulation on the selected surface, making them useful for appropriately controlled treatment of welds and heat-affected zones.
Anopol supplies several products for these applications:
Paste GP: A transparent pickling gel for controlled localised application.
Paste GS: A transparent gel developed for removing weld burn and heat tint.
Paste PNO: A white pickling gel for weld oxide and discolouration removal.
These products are intended for specialist industrial use. The suitability of each formulation depends on the stainless steel grade, oxide condition, application method and approved processing instructions.
Localised treatment must also account for neighbouring materials, surface drainage, rinsing and collection of contaminated residues.
Pickling pastes can contain highly hazardous acids, including hydrofluoric acid. Appropriate chemical risk assessments, engineering controls, training and emergency arrangements are essential.
5. Passivation Chemistry: Supporting Stainless Steel Corrosion Resistance
Passivation is frequently misunderstood as the application of a protective coating.
In reality, stainless steel already possesses the ability to form a passive oxide film.
Chemical passivation is a controlled treatment intended to remove certain surface contaminants, particularly free iron, and promote a suitable passive surface condition.
Unlike pickling, conventional passivation is not intended to remove substantial oxide scale or significantly alter the component's dimensions.
When Is Passivation Appropriate?
Passivation may be specified following machining, fabrication or cleaning where the surface is already substantially free from scale and heavy contamination.
It is particularly relevant where free iron introduced during manufacturing could otherwise produce rust staining or initiate localised corrosion.
Passivation may also form part of a documented manufacturing process where the finished component must satisfy an agreed surface treatment specification.
Anopol supplies Solutions PA, a chemical passivating solution, and Paste PA, a locally applied passivating product.
The exact treatment sequence must be selected according to the component, alloy and specification.
A critical distinction is that passivation cannot reliably compensate for inadequate removal of heavy weld oxide or chromium-depleted surface material.
Where those conditions exist, pickling or another suitable preparatory treatment may be required first.
6. Surface Testing: Verifying Treatment and Material Identification
Visual inspection is valuable, but appearance alone cannot establish that stainless steel is free from surface contamination or that the correct material grade has been supplied.
Chemical test kits can provide additional information during manufacturing and inspection.
Detecting Free Iron Contamination
Free iron may be introduced through contact with carbon steel tooling, grinding particles, workshop equipment or other fabrication operations.
These particles can corrode independently of the stainless steel substrate, creating visible rust staining and potentially contributing to localised corrosion problems.
Anopol's Ferotest is designed to identify free iron contamination on stainless steel surfaces.
Such testing can support inspection following cleaning or passivation.
However, a free iron test is not a complete measurement of corrosion resistance. Results must be interpreted within the scope and limitations of the test method.
Distinguishing 304 and 316 Stainless Steel
Material identification is another important consideration.
Grade 316 stainless steel typically contains molybdenum, which contributes to improved resistance to certain forms of localised corrosion, particularly in chloride-containing environments.
Grade 304 does not normally contain an intentional molybdenum addition.
Anopol's Molytest is designed to help distinguish between 304 and 316 stainless steels.
This can provide a useful screening method during fabrication and inspection.
However, a chemical spot test should not be treated as a substitute for full material certification or quantitative alloy analysis where formal grade verification is required.
7. Process Control: Why Chemical Selection Is Only Part of the Equation
Selecting an appropriate chemical formulation is an important first step, but consistent industrial surface treatment also depends on controlling the complete process.
A properly designed treatment operation must consider the condition of the incoming component, the sequence of processing stages and the requirements of the finished surface.
Key considerations include:
Material identification: Confirming the stainless steel grade and any relevant restrictions before selecting treatment chemistry.
Surface preparation: Removing oils, grease and other contaminants that could interfere with treatment.
Chemical condition: Monitoring relevant bath parameters and maintaining solutions in accordance with the supplier's technical instructions.
Process consistency: Controlling treatment conditions to avoid incomplete processing or unnecessary attack on the substrate.
Rinsing: Removing residual treatment chemicals and dissolved contaminants to prevent staining or subsequent corrosion.
Inspection and testing: Using appropriate visual, chemical or other specified acceptance methods to verify the finished condition.
Effluent management: Ensuring treatment residues and contaminated rinse waters are managed through suitable waste treatment and disposal arrangements.
The correct process will vary depending on the chemistry, alloy, component geometry and applicable specification.
For organisations introducing in-house surface treatment, these factors should be considered during plant design rather than after installation.
8. Chemical Safety and Responsible Industrial Processing
Industrial surface treatment chemicals can present significant hazards.
Depending on the formulation, these may include corrosive liquids, toxic substances, hazardous vapours and contaminated process residues.
Chemical handling and processing in the UK must be supported by suitable risk assessments under the Control of Substances Hazardous to Health Regulations (COSHH).
Manufacturers should also consider chemical compatibility, storage arrangements, ventilation, operator training, emergency procedures and the appropriate treatment of waste streams.
The relevant Safety Data Sheet provides essential information on the hazards associated with each product, but it does not replace a site-specific risk assessment.
For pickling processes involving hydrofluoric acid, additional specialist precautions are necessary because exposure can cause severe injury and systemic toxicity.
Safe operation therefore requires more than selecting an effective chemical. The entire treatment system must be engineered and managed appropriately.
9. Choosing the Correct Chemical Treatment System
There is no single chemical product suitable for every stainless steel surface treatment requirement.
The correct approach depends on what needs to be removed, what surface condition must be achieved and how the component will be used.
For example, a machined stainless steel component contaminated with cutting oil may require degreasing before any subsequent treatment.
A welded fabrication showing significant heat tint may require pickling to remove oxide scale and chromium-depleted surface material.
A clean precision component with free iron contamination may benefit from an appropriately specified passivation treatment.
Where improved micro-smoothness, cleanability or surface appearance is required, electropolishing may be the more suitable process.
In some applications, a sequence of treatments will be necessary.
The most effective approach is to define the required surface condition first, then select the chemistry and processing method capable of achieving it.
Specialist Surface Treatment Chemistry from Anopol
Anopol supplies a comprehensive range of industrial chemicals for electropolishing, pickling, passivation, degreasing and stainless steel inspection.
The range supports manufacturers, fabricators and organisations carrying out their own surface treatment operations.
Alongside chemical supply, Anopol provides technical advice on treatment selection, processing equipment and the practical requirements of industrial surface finishing.
Whether the challenge involves weld oxide removal, electrolyte selection, surface contamination or establishing a controlled in-house treatment process, selecting the correct chemistry is essential.
The performance of stainless steel begins at the surface. Understanding and controlling that surface is where specialist chemical engineering makes the difference.
Explore Anopol's chemical products or contact the technical team to discuss your material, application and surface treatment requirements.